Buying Guides
Box Opening Details That Signal Quality at the Shelf
Box opening details for rigid boxes: thumb notches, ribbon pulls, gate flaps, anchor engineering, and the small mechanics that make a lid feel expensive.
Opening
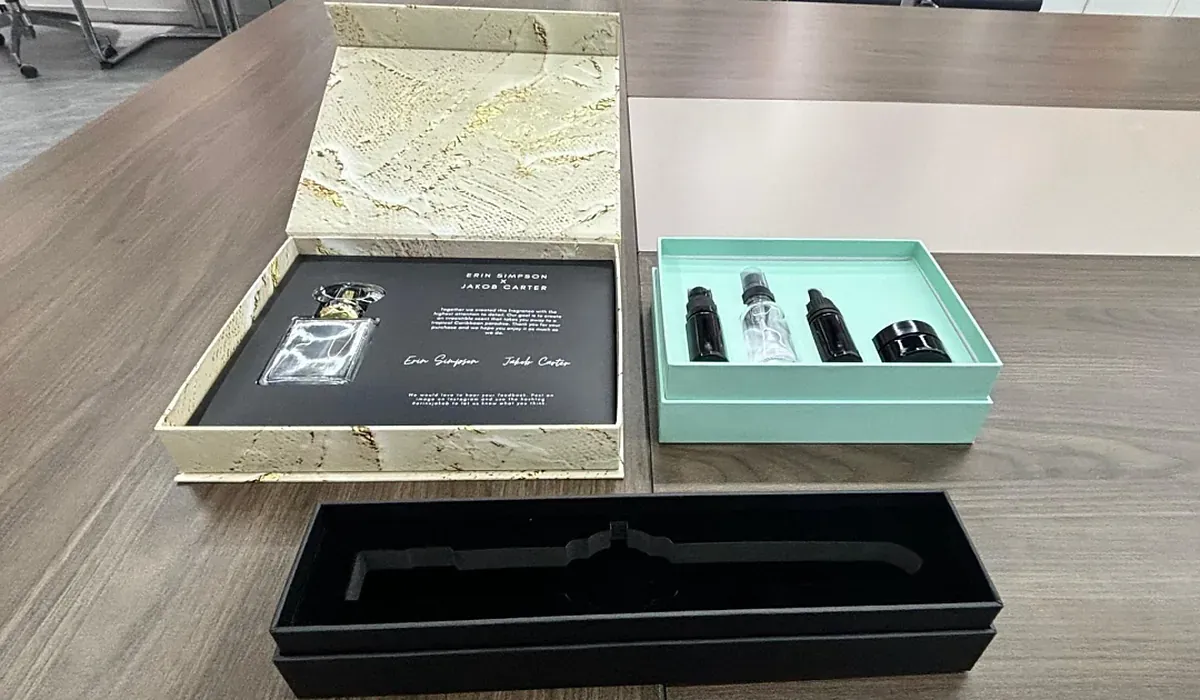
Customers judge a box in the first centimeter of the lift, long before they see the product. Box opening details, the thumb notch, the ribbon pull, the gate flap, decide whether a lid starts smoothly or fights the hand, and that single moment weighs more in perceived quality than most of the finish work around it.
This guide covers the small mechanics that open a box: placement, anchors, hinge geometry, durability and the wholesale terms behind them.
The sections below follow the checks our structure and inspection teams run on every detail that a hand will touch.
Why Openings Signal Quality
Opening is the one moment the customer performs rather than observes, and performed moments read as truth. A lid that needs fingernails, a notch that catches skin, a ribbon that tears its anchor all whisper cheap regardless of how good the print looks. Smooth mechanics whisper the opposite. Buyers should treat opening behavior as a specification, not a detail: we prototype it, cycle it and inspect it like any other feature, because it is the part of the box every single customer will use and remember.
A 60-day guarantee backs each shipment, which is why keeping the delivery date and sample reference matters when a claim is raised.
Thumb Notches: Placement and Size
A thumb notch looks trivial and behaves precisely. Placement decides everything: too low and the hand presses into the interior, too close to the edge and the lid span weakens, too hidden and the customer defaults to prying with fingernails. We place notches at the natural grip point for the box size, size them to a thumb rather than to a drawing default, and die-cut them cleanly so the edge reads smooth in a fingertip sweep. The notch is also a teaching device: it tells the customer where the opening begins without a word.
Ribbon Pulls: Anchor Engineering
A ribbon pull earns its elegance through invisible engineering. The tail passes through a slot and bonds to the board behind the liner, so the pull load lands on structure rather than on the wrap, which is why anchored pulls survive thousands of openings and glued-on ones fail within weeks. Slot position matters too: placed where lid flex is lowest, the ribbon starts the lid along its natural hinge line instead of twisting it. We cycle pulls on samples until the anchor proves itself, because a ribbon that fails at the counter is worse than no ribbon at all.
Gate Flaps and Hinge Geometry
Gate flaps turn an opening into a small ceremony, common on deep boxes and presentation cases where the front panel folds down to reveal the interior. The feel lives in hinge geometry: crease score depth, board caliper at the fold and the flap's own weight decide whether it glides or snaps. We score to the structure rather than to a standard, because a flap that stands open on its own invites inspection while one that flops closed hides the product again. Fabric-hinged and paper-hinged versions each suit different weights, and sampling settles the choice.
Lift Tabs and Finger Ledges
Where notches and ribbons do not suit the design, lift tabs and finger ledges carry the same job. A tab can be a shaped piece of the liner rising through a slot, a leatherette tongue bonded to the tray, or a ledge formed where the inner tray meets the wall. The discipline is the same: load lands on structure, edges finish smooth, and the grip point sits where hands naturally go. Tabs that double as product handles earn double duty, but they must survive the pull test as structure first and decoration second.
Magnets and Closure Feel
Magnetic closures change how a lid ends its travel, and the closing click is the partner of the opening feel. Magnet strength should match lid weight: strong enough that the closure feels confident, gentle enough that the lid opens with one hand. Alignment matters more than strength, since offset magnets let lids sit crooked on the shelf, which reads as defect rather than design. We set magnet positions from the structure model and check closure feel on loaded samples, because an empty lid closes differently from one carrying product, and the customer always meets the loaded version.
The First Centimeter of the Lift
Every opening detail serves the same moment: the transition from closed to moving. A smooth start needs deliberate resistance design. Vacuum and friction hold lids shut on deep boxes, so the detail must overcome that grip without violence, which is why deep structures get notches, ribbons or ledges while shallow ones can rely on a simple lip. We describe this to clients as the resistance curve: how force builds from rest to full travel, and where the hand wants help. Details placed along that curve make any lid feel lighter than it is.
Matching Details to Box Depth
Depth decides which details work. Shallow trays open easily with a simple notch or a finger ledge, and adding ribbon there can feel theatrical. Deep boxes and tall lids need help: a ribbon pull to start the lift, a thumb ledge placed at the balance point, or a gate flap that opens the front instead of fighting the top. Deep structures also concentrate stress at the rim where details anchor, so anchor points get reinforcement behind the liner. We choose details per structure at the dieline stage, because retrofitting an opening aid after tooling costs twice.
Durability: Repeated Opening Cycles
Opening details are the most cycled feature on any box, and durability testing belongs at sampling. We cycle lids through a week of simulated use: notches swept by thumbs, ribbons pulled at counter force, gate flaps folded through their travel, magnets closed against load. Wear shows at anchors first, then at score lines, then at notch edges where wrap fibers fuzz. Details that pass the cycle arrive at retail looking new and stay that way through the season. Buyers should ask any factory how details are cycled, because the answer predicts the second month on the counter.
Board Builds and Wrap Weights
Details live on structure, and structure follows the same discipline as every rigid program. The standard build wraps 1200 g greyboard with 157 g art paper laminate, and slots, notches and anchor points are engineered into the board rather than cut as afterthoughts. Anchor reinforcement sits behind the liner where pulls land, and notch edges are sealed so laminate fibers never fuzz under a thumbnail. We check every opening detail on the wrapped sample, because a slot that cuts cleanly on bare board can still fray once the wrap is on.
Lighter Structures for Volume Programs
Opening details adapt to lighter builds without losing their function. Sleeves and covers built from paperboard in the 300–500 g range take thumb notches and finger ledges naturally, and die-cut pull slots work well where ribbon anchors would overload thin walls. Weight drops, but the resistance curve logic stays: even a light sleeve needs a defined start point or customers will pinch and tear. We match detail weight to structure weight, recommending full rigid mechanics for presentation pieces and simpler die-cut answers for volume retail.
Accessibility and Inclusive Design
Opening details are where inclusive design hides in plain sight. Arthritic hands, gloved hands and customers carrying bags all meet the same notch, and a grip point sized generously serves all of them without a word on the box. Ribbon pulls help anyone who cannot generate leverage, and gate flaps open wide products without two-handed fights. We size details for the harder case by default, because nobody has ever complained that a notch was too easy to use. Accessibility here costs nothing at volume and widens the audience quietly.
Sustainability Notes
Opening details can support the environmental story rather than complicate it. Ribbon tails bond mechanically rather than with tapes, magnets are seated for removal at end of life, and die-cut notches replace plastic pull tabs entirely. We pair detail programs with FSC-ready boards and water-based coatings on request, and a paper-only opening system keeps the whole box in one recyclable stream, which simplifies claims. Where ribbons serve the design, we choose widths and anchor methods that let the detail be cut free cleanly, and we say so in the project file.
Sampling With Real Products
We cut a pre-production sample in about 5 days once structure and artwork are agreed, and opening details should be judged with the box loaded. Empty lids lie about resistance: a notch that works unloaded can vanish under vacuum once product sits inside. Open the loaded sample twenty times, sweep the notch edge with a fingertip, pull the ribbon at real force, and hand the box to someone who has never seen it, then watch where they reach. One revision round is normal, and approval locks detail geometry for the run.
Production Terms and Deposit Flow
After approval, production runs 10-20 working days depending on detail complexity and finish work. Custom programs start at 100 pcs, which suits boutique labels and department store pilots alike. Payment runs on a 30% deposit with the balance before shipment, and the approved sample governs notch geometry, anchor method and closure feel for the whole run. Lead time stretches when details combine with gate flaps or magnetic alignment, so mechanics are confirmed at quotation. Reorders reference the locked project file and retained first articles.
Carton Packing for Detailed Structures
Opening details create protrusions and stress points, so packing protects them specifically. Where size allows, cartons pack at 100 pcs per master carton with weight held under 22 kg, boxes laid flat with ribbon tails tucked inside and gate flaps closed so protruding parts never catch on neighbors. Void fill supports rather than fills, and orientation marks keep structures upright through warehouses. Buyers checking arrivals should cycle one lid per carton against the retained sample, because transit pressure finds anchor weaknesses faster than any bench test.
Inspection of Opening Mechanics
Every order ships under AQL inspection with checks weighted to opening risks: notch edge smoothness, ribbon anchor pull strength on sampled units, gate flap score integrity through full travel, magnet alignment and closure feel against the first-article standard, and fuzzing at slot edges where the wrap was cut. Inspectors cycle lids on sampled units rather than judging them closed. Lots that miss the acceptance threshold are reworked before release, and inspection records travel with the shipment for the client's quality file.
Buyers Who Specify Mechanics
Jewelry labels, spirits houses, subscription brands and corporate gift teams commission box opening details most often, and their priorities differ. Jewelry teams want one-handed openings that never disturb a staged interior; spirits brands want a start-of-lift moment that matches the price; subscription programs want mechanics that survive monthly cycling without tearing. What they share is the need for a factory that engineers anchors behind the liner, cycles details at sampling and treats the first centimeter of the lift as a specification.
Factory Setup and Market Reach
The plant covers 5,000 m² with 100 staff across die-making, printing, wrapping, assembly and inspection, and annual output runs near US$10 million. We have operated since 1998, and opening mechanics repeat in our die library, which keeps reorder costs predictable and details identical to the launch run. Programs ship to 80+ countries, the case record spans 50+ brands across jewelry, spirits and gifting, and the project log includes 1,000+ cases of custom packaging. Bring box dimensions and handling scenarios, and we will return detail options with honest trade-offs.
Frequently Asked Questions
Where should a thumb notch sit so the lid lifts without pressing the interior?
At the natural grip point for the box size, placed where the hand reaches without bending over the opening. Notches set too low force fingers into the interior, disturbing staged product before it is seen. We position notches from the structure model, size them to a thumb rather than a default, and verify on a loaded sample, because vacuum and product weight change where the grip actually wants to be.
Why do some ribbon anchors tear the wrap after repeated pulls?
Because the pull load lands on the wrap instead of on structure. Tails glued to the liner face transfer every tug into the laminate, which peels from its anchor point within weeks. Proper anchoring passes the ribbon through a slot and bonds it to the board behind the liner, so the load reaches structure first. We cycle pulls at sampling until the anchor proves itself under real force.
Does a finger notch weaken a narrow lid span?
It can, when the notch sits too close to the span's center. A notch removes material exactly where lid flex is highest, so placement shifts toward supported zones near corners or reinforced rim areas. We size and position notches against the structure model, then check lid stiffness on the wrapped sample. Where the span is genuinely narrow, a ribbon pull or ledge serves better than a deeper notch.
What hinge geometry makes a gate flap feel smooth instead of stiff?
Score depth matched to the flap's weight and board caliper. A shallow score fights every fold, while one cut to the structure lets the flap glide through its travel and rest open where the design wants it. Fabric hinges suit heavier flaps, paper hinges suit lighter panels. We prototype hinge options on the actual structure at sampling and choose by feel, because flap weight changes once product sits inside.
Can a notch be die-cut into the liner without showing on the outer face?
Yes, when the notch is planned into the board before wrapping rather than cut afterward. Die-cutting the structure first means the wrap turns into the recess cleanly, and the outer face stays uninterrupted because the opening lives in the liner geometry. Cutting through wrap exposes cut fibers at the outer face. We plan notches at the dieline stage, and the wrapped sample confirms the face reads clean.
How does a satin pull change the perceived weight of a deep lid?
A pull redistributes effort: the hand draws along the lid's natural hinge line rather than prying against vacuum, and the lid reads lighter. Ribbon also sets the opening pace, starting the lift smoothly rather than with a jerk, which reads as elegance. Deep lids benefit most because resistance builds fastest there, and a pull placed at the balance point turns a two-handed fight into a one-handed gesture.
Conclusion
The first centimeter of the lift is the cheapest premium available: box opening details cost little, get used by every customer, and decide whether craftsmanship is felt or merely claimed. Place notches at natural grip points, anchor pulls to structure rather than wrap, score hinges to the flap's own weight, and cycle everything on loaded samples before approval. BoxesChina engineers opening mechanics into the dieline and inspects them under AQL. Send box dimensions and handling scenarios, then Request a Wholesale Quote, and our team will return detail options, anchor plans and factory pricing for lids that start as smoothly as they look.