Buying Guides
Delta E Color Acceptance: Setting a Tolerable Print Color Standard
How to set a delta E colour tolerance for packaging: which formula, which thresholds hold up, how to measure, and how to write acceptance into a PO.
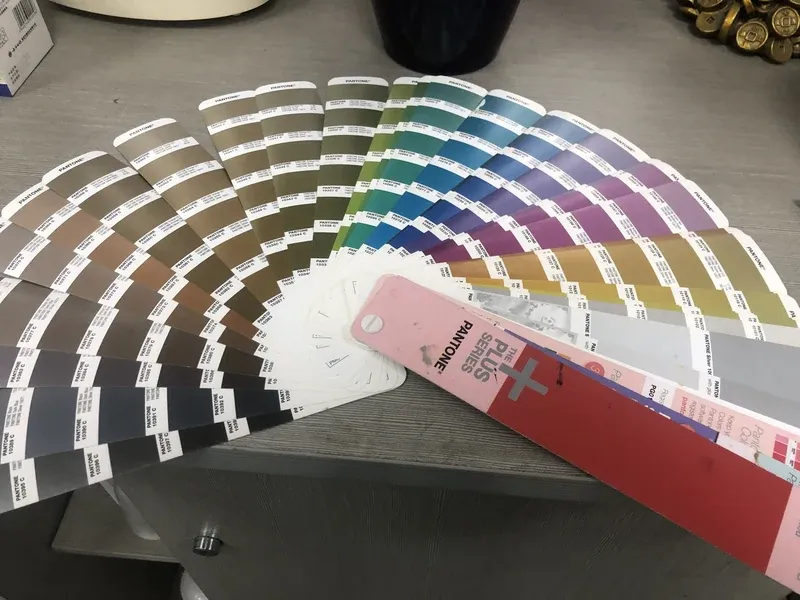
Delta E (ΔE) is a number that expresses how far one printed colour sits from a reference colour in a perceptually organised colour space, and it is the only practical way to write a colour acceptance criterion that a press operator, a converter, and a brand owner can all agree on. A ΔE of about 1 is at the edge of what most people can see; by roughly 2 to 3 it is visible side by side but not across a room; above about 5 the difference reads as a different colour. Those thresholds are orientation, not law — the right limit depends on your brand, the substrate, the print process, and what your customer will accept.
The trap is that ΔE is not one number. There are several formulas in use, they do not return the same value for the same pair of colours, and a tolerance agreed without naming the formula is not a tolerance at all. Two suppliers can both report "ΔE 2.1" and both be right while describing two different print results.
This guide covers how the number is produced, which thresholds are defensible, how to agree a colour standard with a printer, and how to build acceptance into a purchase order so that a reprint conversation has an answer. Instrument settings, formulas, and reference conditions are standardised but revised; confirm the current version of any standard you cite with your laboratory and your print supplier in writing.
What the number actually represents
Colour measurement converts reflected light into three coordinates in a colour space — lightness (L), and two chromatic axes (a and b*). A spectrophotometer reads the printed sample and the reference, converts both, and computes a distance between them. ΔE is that distance.
Because "distance" in a colour space is not the same as "difference the eye notices", the industry has produced successive formulas:
ΔE76 — a straight Euclidean distance in Lab*. Simple, still widely quoted, and known to over-weight differences in saturated colours; ΔE94 — introduces weighting so that hue and chroma differences count differently from lightness, and so that the acceptable difference shrinks as colours become more saturated; ΔE2000 — a more elaborate model with additional corrections for hue rotation and the blue region, generally considered the closest to visual perception of the three.
The consequence is practical, not academic. For a mid-tone brand colour, ΔE76 and ΔE2000 might differ by a factor of two. If your purchase order says "ΔE ≤ 2" and the printer measures with a different formula than the one your brand team used, you will have a dispute about arithmetic rather than about print quality.
Behind that spec, We support 50+ private-label brands as their packaging partner. We have delivered 1,000+ case projects across the catalog. Product ships to 80+ countries through our export desk.
So the first line of any colour specification is: which formula. Write it. Ours name the formula, the illuminant (D50 is the common reference for print evaluation), the standard observer (2° or 10°), the instrument geometry, and the measurement backing.
Setting a colour standard for a new pack? [Send us your reference and target substrate →] and we will return a measured colour report with the formula, illuminant, and instrument conditions stated, plus the tolerance we would propose per colour.
Which thresholds hold up
The widely used orientation scale, in ΔE2000 terms:
ΔE (approx.) — What a trained observer sees — Typical use. Under 1 — Not distinguishable — Instrument-level match; often uneconomic in production. 1 to 2 — Perceptible on close comparison — Achievable target for a well-controlled spot colour. 2 to 3.5 — Perceptible at a glance, side by side — Common working acceptance band for brand spot colours. 3.5 to 5 — Clear difference, but same colour family — Process builds, large solid areas, secondary graphics. Above 5 — Reads as a different colour — Reject for brand colours.
Three qualifications before anyone copies that table into a contract.
Substrate drives the achievable floor. An uncoated recycled board with visible fibre and a mottled surface will not hold the same tolerance as a coated white board. If you write a coated-board tolerance against an uncoated substrate, you will spend the life of the pack rejecting compliant work.
A detail from the workshop: Rigid boxes use 157 g face stock over 1200 g greyboard. Folding cartons are specified in 300-500 g board. Bulk decoration uses offset printing for colour stability.
Area drives perception. A ΔE of 3 on a 5 mm logo rule is invisible. The same ΔE across a 200 mm solid panel is obvious. Large solids therefore need tighter process control even when the numeric tolerance is the same — or a slightly looser tolerance with a rule about mottling and density variation, which is the actual defect customers notice.
Process colour behaves differently from spot colour. A four-colour build is a stack of dots; small ink film variations move the result more than they would in a flat spot ink. Where the brand colour matters, a dedicated spot ink is usually cheaper than the quality control needed to hold a process build.
Measuring so the number means something
A ΔE value is a measurement result, and like any measurement it depends on how it was taken. Four variables do most of the damage:
Instrument geometry. A 45/0 or 0/45 instrument and a sphere instrument do not see textured or glossy surfaces the same way. Compare like with like; Illuminant and observer. D50 with a 2° observer is a common print convention. D65 with 10° is common elsewhere. Mixing them shifts the number, especially in blues and yellows; Sample presentation. Ink on a curved carton panel, a corrugated flute, or a creased fold reads differently from a flat drawdown. Measure what the customer will see, in the orientation they will see it; Backing and opacity. A thin printed sheet measured over a white backing and over a dark one gives two answers. Specify an opaque backing or multiple layers.
Then there is the question of how many readings and where. One reading on one spot proves nothing about a print run. A defensible protocol takes multiple readings across the run, at defined locations, and reports the mean and the spread. If your supplier only reports a single best reading, you are being shown a demo, not a result.
Where the reference comes from
Every ΔE needs a reference, and the reference is where projects quietly go wrong. Three options, in descending order of reliability:
A measured physical standard — a signed, dated printed sheet retained by both parties, re-measured when the job is re-run. This is the only version that survives staff turnover; A numerically defined target — Lab* values agreed in writing, usually derived from a brand colour specification. Reliable if the ink and substrate can reach it, which is a question to settle at sampling; A screen or a photograph — not a reference. Monitors are uncalibrated, viewing conditions vary, and a phone photo of a box is a mood board, not a specification.
Whichever you choose, the standard has to state the substrate. A colour target that does not name the board is a target that cannot be met or missed, only argued about.
The visual side of approval — booth conditions, metamerism, and how a signed standard is managed — is covered in D50 light booth color approval packaging. Read the two together: ΔE is the instrument's opinion, and the booth is the eye's.
Asymmetric tolerances: the part that saves money
A single ΔE ceiling treats every direction of error as equally bad. They are not.
Lightness errors are usually the most visible on a solid panel, because the eye adapts less to a lightness shift than to a small hue shift across a fold; Hue errors matter most on brand colours, because the brand is recognised by hue rather than by exact lightness; Chroma errors in the direction of greyness read as "cheap" even when the ΔE is modest, especially on rich reds and deep blues.
A more useful specification therefore sets an overall ΔE limit plus direction-specific limits — for example, a maximum lightness deviation that is tighter than the overall limit, and a hue-angle tolerance for the brand colour. Press operators find this easier to act on too, because "the yellow is drifting green" is a corrective instruction, while "ΔE 3.4" is only a verdict.
Building acceptance into the purchase order
A workable colour clause has six parts:
Reference identity — signed physical standard and its date, or numeric target values, plus the substrate named; Measurement conditions — instrument geometry, illuminant, observer, backing, and the number and location of readings; Formula — named explicitly, with the software version if the parties are being thorough; Limits — overall ΔE per colour, plus direction-specific limits for the brand-critical ones; Acceptance gate — first-off approval measured against the standard before the run continues, and a sampling rule for the rest of the run; Remedy — what happens when a reading exceeds the limit: re-make, sort, accept with a concession, or reject. Without this line, the limit is decorative.
Two supporting documents make the clause enforceable in practice: a per-colour table rather than a single job-wide number, and a record of the measured readings attached to the shipment. Our notes on
Digital proof vs wet proof
explain why the proof stage cannot substitute for a measured press sheet, and Packaging artwork check
covers the artwork controls that prevent a colour change nobody intended.For context, We return a free digital proof in about 5 days. Standard terms are 30/70 (deposit / before shipment). MOQ starts at 100 pcs per SKU for most formats.
Mini story: two suppliers, two formulas
A US skincare brand we will call Lumen & Larch had a signature sage green on a coated folding carton. The brand's style guide defined it numerically, and its first Chinese supplier reported ΔE readings in the low twos on every shipment. The packs looked acceptable.
A second supplier, brought in for capacity, reported readings of about 1.2 — better on paper — but the cartons looked visibly duller next to the first supplier's. The brand's packaging manager asked both for their measurement conditions.
Worth pinning down: Roughly 100 staff work across production, prepress, and QC on a 5,000 m2 floor. Our export desk handles documentation and freight consolidation in-house. Annual export value runs above US$10M.
Supplier one had been reporting ΔE76 with a 10° observer on a single reading near the centre of the panel. Supplier two reported ΔE2000 with a 2° observer and nine readings, but against its own internal target, not the brand's numerical standard. Neither was cheating. The numbers simply described different measurements of different references.
The fix was a two-page colour annex: one formula, one illuminant and observer, one instrument geometry, one signed physical standard held by both parties, and nine defined reading positions with a per-colour limit and a direction-specific lightness cap. Reprint disputes at the brand dropped to roughly one a year, and both suppliers started reporting numbers that could be compared.
Mini story: the kraft box that could not hit the target
A Dutch coffee brand we will call Kade Koffie moved a retail carton from coated white board to an uncoated kraft board for a more natural look. The artwork was unchanged and the colour target was unchanged.
One practical note: Cartons pack 100 pcs and stay under 22 kg for courier limits. We run FSC-ready board lines and can specify certified stocks on request. Finished goods are inspected to AQL standards before release.
The first production run measured ΔE values well outside the previous tolerance on the brand's deep teal. The printer was not at fault: uncoated kraft has a darker, warmer base and a more open surface, so the same ink film reads differently and partly sinks into the sheet. The brand's numeric target had been established on coated board.
Two options existed. Chase the original target with heavier ink coverage on an absorbent sheet — expensive, slower to dry, prone to set-off — or re-establish the target on the new substrate and accept a slightly warmer teal as the new standard. The brand chose the second, re-issued the standard with the substrate named, and reset the tolerance to a limit the sheet could hold consistently.
The lesson is the one worth carrying into every substrate change: a colour standard is a standard for a specific ink on a specific board. Change either and you have a new standard to agree, not a failure to blame.
Common mistakes
Agreeing a ΔE limit without the formula. The same print can pass or fail depending on the model used.
Using one number for the whole job. Brand spots, tints, and process builds need different limits.
Measuring one reading on a flat drawdown. Production is a run on a real substrate with real texture.
Comparing across substrates. Coated white, uncoated kraft, and recycled board are three different colour problems.
Treating the proof as the standard. A proof predicts; a press sheet measures. Approve a measured physical standard.
From the factory floor, Mass production runs in 10-20 working days after proof sign-off. Every order carries a 60-day quality guarantee. Our plant has made custom packaging in Dongguan, China since 1998.
No remedy clause. A limit without a consequence is a suggestion.
Ignoring metamerism. Two samples can match under one light and diverge under another — which is how a pack that passed in the factory looks wrong in a store. The booth protocol handles that; the instrument alone will not.
Colour acceptance checklist
Reference standard identified: signed physical sheet with date, or numeric Lab* target; Substrate named in the standard, and the target re-established when the substrate changes; Formula named: ΔE76, ΔE94, or ΔE2000, stated explicitly; Measurement conditions fixed: illuminant, observer, instrument geometry, backing; Reading protocol defined: number of readings, locations, and how spread is reported; Per-colour limits set, with direction-specific caps for lightness and hue on brand colours; First-off approval gate written into the run, measured against the standard before continuing; Remedy clause agreed: re-make, sort, concession, or reject, with the decision owner named.
Need a colour standard both sides can measure? [Request a printed sample with a measured colour report →] boxeschina has delivered 1,000+ custom packaging projects to buyers in 80+ countries since 1998, with ~5-day free samples, low-MOQ reorders from 100 pcs, and transparent quoting with no hidden fees.
Conclusion
ΔE turns a subjective argument into a measurement, which is exactly what a custom packaging project needs — provided the measurement is specified as carefully as the colour. Name the formula, fix the illuminant, observer, geometry, and backing, define how many readings count, set tolerances per colour with direction-specific caps for the brand-critical ones, and attach the whole thing to a signed physical standard on a named substrate.
Then treat the number as a tool rather than a verdict. A ΔE reading tells you a difference exists and roughly how large it is; the booth tells you whether a customer will see it; the failure mode tells you what to change. A print project that has all three is a project that can be reprinted without a negotiation.
Confirm the current version of any standard you cite, and the measurement conditions your lab or printer will apply, in writing before the tolerance goes into a purchase order.
FAQ
What is a good ΔE for packaging print? It depends on the colour, the substrate, and the print process. As orientation in ΔE2000 terms, under about 2 is a good target for a controlled spot colour on coated board, roughly 2 to 3.5 is a common working acceptance band, and differences above about 5 read as a different colour. Agree limits per colour rather than one per job.
Why do two suppliers report different ΔE for the same print? Usually because they used different formulas, different illuminants or observers, different instrument geometry, or different references. ΔE is not comparable unless the measurement conditions and the reference are identical.
Should I specify ΔE76 or ΔE2000? ΔE2000 correlates best with visual perception, and ΔE76 remains common in older specifications. What matters most is that both parties use the same one and that the limit was set for that formula. If you are writing a new specification, name the formula explicitly.
Can I accept a colour based on a digital proof? A proof predicts how the job should print; it is not a measurement of the printed result. Approve a measured press sheet or a printed sample as the physical standard, then measure production against it.
Why did my colour fail after changing to recycled board? Different furnish, whiteness, and surface absorbency change how ink reads. A target set on coated white board is not transferable to an uncoated or recycled substrate without re-establishing the standard and re-testing the achievable tolerance.
How many readings should be taken? Enough to describe the run, at defined locations, with the spread reported. A single reading demonstrates a possibility, not a result. Agree the protocol in advance so the data can be compared across shipments.