Buying Guides
Custom Heart-Shaped Boxes: Where the Curve Breaks the Spec
Custom heart-shaped boxes fail at the concave notch, lobes, and point. Learn the geometry, wrapping method, board caliper, lid fit, insert cavity, and the production-built sample gate.
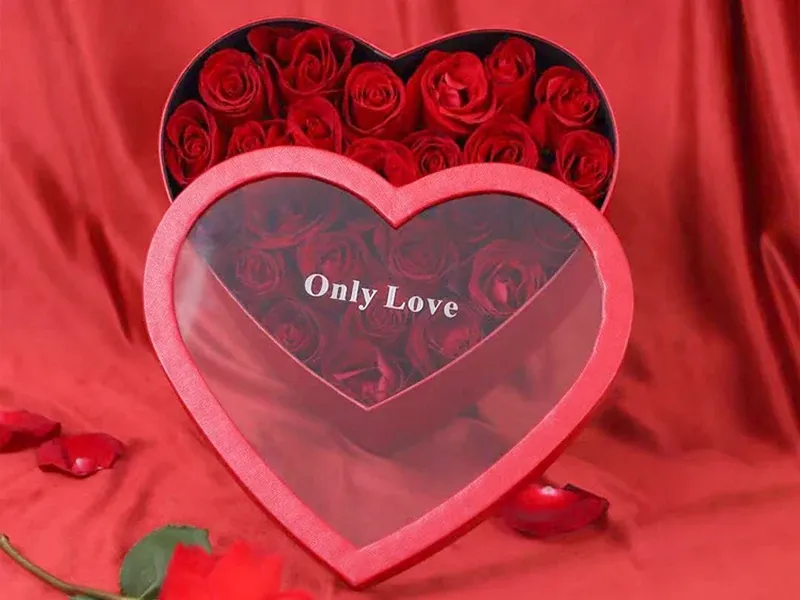
A heart-shaped box is a rigid structure with two concave lobes and a sharp point. Those three features are where wrapping paper wrinkles, greyboard shows through, and lids stop fitting. Sourcing one successfully is less about the shape and more about how the converter handles the curve: the wrap method at the lobes, the board caliper and the seam, the lid-to-base tolerance at the point, and the insert that has to follow a non-rectangular cavity. Write those as named spec lines and approve a production-built sample, not a hand-made one.
A buyer we'll call Nadia ordered heart boxes for a Valentine's launch. The hand-made sample was flawless. The production run arrived with visible wrinkles at the inner notch between the lobes, a fine grey line showing at the bottom point, and a lid that rocked. The supplier had built to the approved shape; what had never been specified was how the wrap was turned at the concave area. This guide covers the geometry, the wrapping method, the tolerance, and the receiving checks for custom heart-shaped boxes.
The three geometry problems
A rectangle has straight edges and square corners. A heart does not. That changes what a converter has to do with paper and board.
Feature — What goes wrong there — What to specify. Inner notch between the lobes — A concave curve; wrap paper has to compress, so it pleats or wrinkles — The wrapping method at concave sections and any relief cuts. Outer lobes — Two convex curves with a changing radius — Wrap grain direction and the overlap or seam location. Bottom point — An acute corner; board edge can show, wrap can tear — Corner treatment, board edge coverage, and a point-radius decision. Lid-to-base fit — No straight edge to register against — A fit tolerance and a defined check at the point and both lobes.
The first row is the one that produces almost all visible defects. Paper does not compress into a concave curve without help. A converter either makes small relief cuts and turns the wrap in sections, or uses a wrap method designed for curved work. Ask which method will be used on the production line and get the answer in writing, with a photo of the notch on a production-built sample.
Want the geometry lines as a spec sheet? [Ask our Dongguan team for the shaped-box RFQ template →] — notch, lobes, point, and lid fit each with their own line, with ~5-day free samples and transparent quoting with no hidden fees.
Board, wrap, and the seam
A shaped rigid box is greyboard wrapped in paper. Those are separate decisions.
Greyboard caliper — state the caliper in mm (and the gsm if your quality team uses both), with a tolerance. A shaped box needs enough stiffness to hold a curve without bowing; see Greyboard thickness rigid box for how caliper and gsm relate; Wrap stock — grade, gsm, and whether it is coated or uncoated. A stock that is too heavy will not turn a tight concave curve cleanly; one that is too light will show the board texture; Wrap grain direction — paper has a grain. State it on the spec, because it decides how the wrap behaves at the lobes; Seam and overlap location — name where the wrap joins and which face it sits on. On a heart there is no obvious "back"; if it is not written down, it moves between lots; Inside face — a lined interior or a turned-in wrap. This is a common silent substitution. See Sbs vs ccnb vs fbb for why the inside colour matters; Corner and point treatment — how the board edge is covered at the acute point, and whether a small radius is applied.
Worth pinning down: Rigid boxes use 157 g face stock over 1200 g greyboard. Folding cartons are specified in 300-500 g board. Bulk decoration uses offset printing for colour stability.
Confirm the current technical values in writing with your own laboratory or quality team. A caliper that works on a rectangular box may behave differently across a curved span.
The wrapping method is the actual product decision
Two converters can build the same heart from the same board and produce different results. The difference is the wrap method at the concave notch.
Ask three questions before tooling:
How is the wrap turned at the inner notch — relief cuts, sectioned turning, or a formed method? Get a written description; Is the wrap applied by hand or on a formed line? A hand-built sample can achieve a curve a production line cannot repeat; What is the acceptance check for the notch — visual under a defined light, or a written criterion agreed with your quality team?.
A point on how we build: We have delivered 1,000+ case projects across the catalog. Product ships to 80+ countries through our export desk. We support 50+ private-label brands as their packaging partner.
The failure modes behind this are covered in
Rigid box wrapping wrinkles
. What matters here is that the method is a spec line, not an implicit skill. If a supplier answers "our workers are experienced", ask again for the method and a production-built sample.Lid-to-base fit has no straight reference
On a rectangular two-piece box you can measure a gap along a straight side. On a heart you cannot. Fit has to be defined at named points.
Write these lines:
Fit at the point, at both lobes, and at the notch — each with an agreed tolerance as confirmed with your quality team; Opening and closing action — how much resistance, and whether the lid rocks or sits flat; A registration reference — since there is no straight edge, name how the lid and base are aligned during assembly; A defined check — close the lid on the production sample and record the result in writing, with a date.
A detail from the workshop: Our export desk handles documentation and freight consolidation in-house. Annual export value runs above US$10M. Roughly 100 staff work across production, prepress, and QC on a 5,000 m2 floor.
A lid that rocks by a small amount on a rectangle reads as a defect; on a heart it is easy to miss until a customer opens it. Approve the fit on a production-built sample, signed and dated, and put the sample ID in the purchase order.
The insert must follow the cavity
A heart-shaped box with a rectangular foam pad inside has an unfilled crescent at each lobe and a gap at the point. The contents shift in transit, and the unboxing looks unfinished.
Specify:
Cavity shape drawn to the internal outline, with a drawing version; Material and density or grade, as agreed with your quality team; Holding mechanism — a shaped cavity, a ribbon tie, or a fitted surround. See Gift box insert choice for the matching method; Clearance around the contents, with the widest point measured including any closure or protrusion. The dimension convention is in How to measure box dimensions; Assembly orientation and a photographed pack-out reference.
Approve one fully assembled sample with the real contents. An empty shell cannot show whether a chocolate or a piece of jewellery sits where it should. The sample-evaluation method is in
How to evaluate packaging sample
.Have a heart-box sample that was hand-built? [Send us the shape and the contents →] — we will mark the notch method and the fit lines before tooling, with low-MOQ custom from 100 pcs and transparent quoting with no hidden fees.
Mini story: the notch that could not be repeated
A buyer we'll call Marcus ordered heart boxes for a confectionery range. The approval sample was made by the most experienced wrapper in the room, with tiny relief cuts at the inner notch that were never drawn anywhere. The production team, working to a cycle time, could not reproduce them.
The run arrived with fine pleats at every notch. Marcus could not claim a deviation: the method had never been in the spec. For the next order he asked for a written description of the wrap method at concave sections, a photograph of the notch from a production-built sample, and a defined visual acceptance check under one light. The second run matched. The skill had not changed. The method had been written down.
Tooling, MOQ, and the sample gate
A shaped die is one-time preparation and should be a separate line with a die ID and the dieline version — see
Custom packaging tooling mold fee
. Many factories run custom work from around 100 pcs, low enough to validate a curve before scaling; see Real low moq custom packaging
.Approve in this order:
A dieline showing the outline, the notch radius, the point radius, seam location, wrap grain, and insert cavity; A production-built shell — not a hand-made one — in the real board and wrap; A lid-fit result recorded at the point and both lobes; A fully assembled sample with the real contents; A signed sample ID, plus the die ID and dieline version, written into the purchase order.
The proof and colour workflow is in
Digital proof vs wet proof
. Sign and date the physical sample; a photo of a hand-made one is not a reference a production line can repeat.In the same brief, Standard terms are 30/70 (deposit / before shipment). MOQ starts at 100 pcs per SKU for most formats. We return a free digital proof in about 5 days.
RFQ lines for a shaped box
Outline geometry — overall L × W × H, notch radius, lobe radii, point radius, in mm with tolerances; Wrapping method at concave sections, grain direction, seam and overlap location, inside face; Board caliper in mm with tolerance, and gsm if used; wrap stock grade and gsm; Lid fit at the point, both lobes, and the notch, with the check method; Insert cavity drawing version, material, holding mechanism, and clearance; Finish list — each process named with its area. A large foil area near the notch is a cracking risk; see Foil stamping vs metallic ink; Quantity tiers, artwork version, and the die ID; Acceptance checks — notch finish, point coverage, lid fit, colour, and assembled fit; A line asking for any unstated assumption as a separate line.
To put numbers on it, Cartons pack 100 pcs and stay under 22 kg for courier limits. We run FSC-ready board lines and can specify certified stocks on request. Finished goods are inspected to AQL standards before release.
The comparison method for the replies is in
Alibaba rfq custom packaging quote
.Receiving checks and failure attribution
Check the three geometry points before stock release. The receiving protocol is in
Quality control checklist packaging shipment
.Failure on arrival — Likely cause — Record to check. Wrinkles at the inner notch — Concave wrap method not specified or not repeatable — Wrapping method line and production sample photo. Grey line showing at the point — Board edge not covered, corner treatment missing — Corner treatment line and point radius. Lid rocks or will not seat — Fit tolerance undefined; no registration reference — Fit lines at point/lobes and the signed sample. Wrap shade differs — Different stock or a fresh proof — Signed sample ID and lighting condition. Contents shift — Rectangular or undersized insert — Cavity drawing version and pack-out photo. Foil cracking near the notch — Foil crossing a flex point — Foil area in mm and artwork version.
On the production side, Our plant has made custom packaging in Dongguan, China since 1998. Mass production runs in 10-20 working days after proof sign-off. Every order carries a 60-day quality guarantee.
Write each difference as a numbered line with a count and the spec clause it touches; ask for a written reply against your line numbers.
Red flags before the deposit
A hand-made sample offered as the approval reference for a shaped box; No written wrapping method for the concave notch; No lid-fit tolerance at the point and lobes — "fits well" is not a check; Seam location unstated, so it moves between lots; A rectangular insert inside a shaped cavity; A large foil area running into the notch with no relief decision; No die ID or dieline version attached to the tooling line.
Pre-Order Shaped Box Checklist
Specify outline geometry in mm: overall size, notch radius, lobe radii, and point radius, with tolerances; Name the wrapping method at concave sections, the wrap grain direction, and the seam/overlap location; State board caliper in mm with tolerance, wrap stock grade and gsm, and the inside face treatment; Define lid fit at the point, both lobes, and the notch, with a written check and a registration reference; Provide an insert cavity drawing version with material, holding mechanism, and clearance around the contents; Confirm the current technical values in writing with your own laboratory or quality team; Approve a production-built shell, a recorded lid-fit result, and one fully assembled sample with real contents; Put the signed sample ID, die ID, dieline version, and a written acceptance check into the purchase order.
Mini story: the seam that moved
A buyer we'll call Aisha reordered a heart box for a second season. The shape, board, and artwork were identical, but the wrap join had moved from the lower point to the outer lobe, where it caught the light in product photos. Nobody had decided to change it; the seam location had never been written down.
She added one line to the master spec — "wrap join at the lower point, on the underside" — and attached a photograph of the approved production sample. Her third season matched the first. Aisha had not found a more careful converter. She had given a decision that used to be implicit a place to live.
Conclusion
A heart-shaped box is a rigid structure with three awkward features: a concave notch, two lobes, and an acute point. Those are where the wrap wrinkles, the board shows, and the lid stops fitting. A hand-made sample hides all three; a production-built one shows them.
Write the outline geometry in mm, name the wrapping method at concave sections, state the board caliper, wrap stock, grain direction, and seam location, and define lid fit at the point and both lobes. Give the insert a cavity drawing version that follows the shape. Approve a production-built shell, a recorded fit result, and one fully assembled sample, then attach the signed sample ID, die ID, and dieline version to the purchase order. Confirm the current technical values in writing with your own quality team. Any figures attached to a quote vary with specification, quantity, route, and the rules in force at the time, and must be confirmed in writing by the supplier.
Start with a shaped-box geometry sheet → Our Dongguan team has delivered 1,000+ custom packaging projects to buyers in 80+ countries since 1998, with low-MOQ custom from 100 pcs, ~5-day free samples, and transparent quoting with no hidden fees.
FAQ
Why do heart-shaped boxes wrinkle at the inner notch? Paper does not compress into a concave curve without help. The converter needs relief cuts, sectioned turning, or a formed wrap method. Ask which method the production line uses and get it in writing with a photo of a production-built sample.
Can I approve a hand-made sample for a shaped box? Not as the sole reference. A skilled wrapper can achieve a curve a production line cannot repeat. Approve a production-built shell in the real board and wrap, plus a recorded lid-fit result.
How do I specify lid fit when there is no straight edge? Define fit at named points — the bottom point, both lobes, and the notch — each with a tolerance agreed with your quality team, plus a registration reference and a written closing check.
What insert works in a heart-shaped box? One drawn to the internal outline, with a cavity version, material, holding mechanism, and clearance around the contents. A rectangular pad leaves unfilled crescents and lets the contents shift.
What belongs in the RFQ beyond the shape? Outline geometry in mm, wrapping method at concave sections, grain direction, seam location, board caliper and wrap stock, lid-fit lines, insert cavity version, finish areas, quantity tiers, and the die ID.