Buying Guides
Rigid Box Manufacturer: Greyboard and Magnetic Closure
Rigid Box Manufacturer: 157g face plus 1200g greyboard, magnetic closures, and UV finish for a luxury unbox that survives repeat handling.
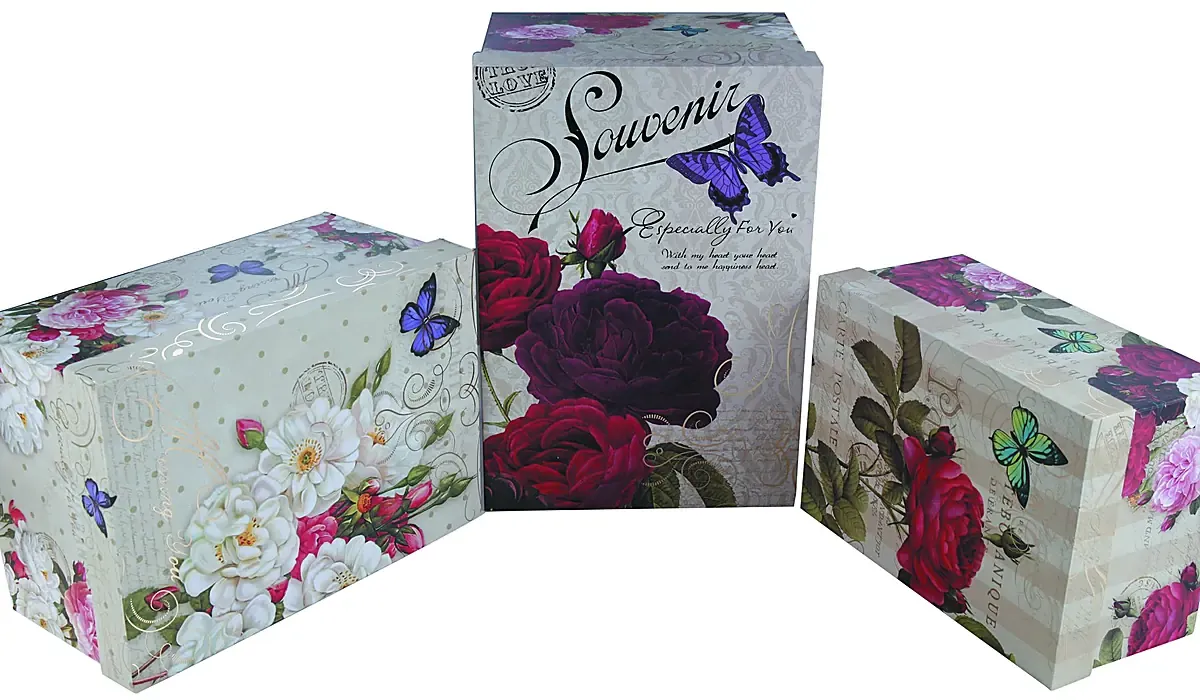
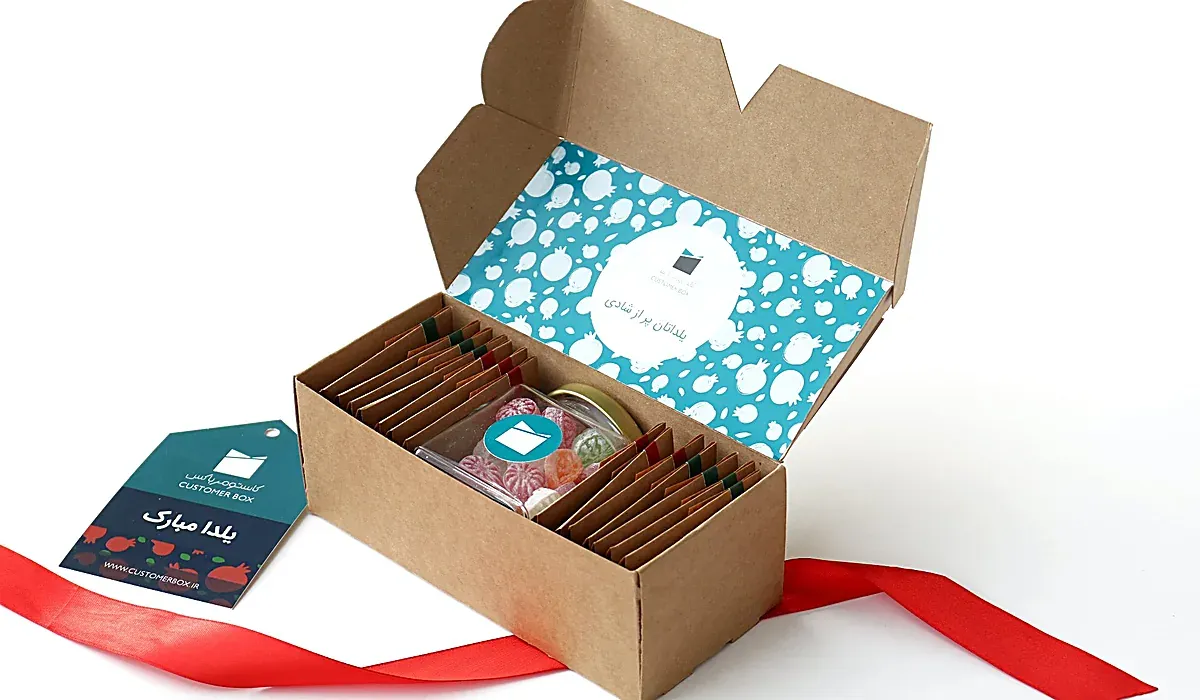
Rigid boxes are a core packaging decision for brands in luxury gifting, electronics presentation, cosmetic sets, jewellery and watch packaging. Sourcing them from a manufacturer rather than a trader gives control over the material, the dimensions, and the finish, and that control is what turns a box from a cost into part of the product experience. A rigid box manufacturer wraps greyboard with printed face paper, and the right partner specs the wrap, the magnet, and the finish as one system rather than separate line items. This guide covers the practical side of buying rigid box manufacturer from a China factory: the materials and grammage that set quality, how custom dimensions are specified, and the order rhythm that keeps a brand in stock through a peak. The intent is to let a buyer brief a supplier with enough detail that the first order is a confident test rather than an expensive guess. When you plan a rigid box manufacturer order, send product dimensions, target market, and a print reference so the factory returns a dieline and a proof quickly.
The hard facts that frame every order are stable: the minimum order starts from one hundred pieces, sampling takes only a few days, and bulk production runs ten to twenty working days. Rigid boxes use 157 gram face paper over 1200 gram greyboard; folding cartons use 300 to 500 gram paperboard. Boxes are packed one hundred pieces per carton kept at or under twenty two kilograms. FSC ready paper is available with chain of custody documents on request, and Manufacturing is based in Dongguan, China, with operations established since 1998. Hold those facts in mind as you read, because they are the constants behind the choices that follow, and they are what let you plan a landed timeline instead of hoping one appears. The rest of this guide breaks each constant into a choice you can make with the factory rather than a number you merely accept.
What Rigid Boxes Are and Who Needs Them
Rigid boxes are a foundational packaging product for businesses that ship luxury gifting, electronics presentation, cosmetic sets, jewellery and watch packaging. A factory that makes them controls the paper, the board, and the print from one site, which is why the manufacturer lane matters more than a trader when volume and consistency are the priority. A rigid box manufacturer wraps greyboard with printed face paper, and the right partner specs the wrap, the magnet, and the finish as one system rather than separate line items. Buyers come to a manufacturer to set the material, the dimensions, and the finish rather than accept a catalogue default, and that control is what turns a box from a cost into part of the product experience.
The applications for rigid boxes span luxury gifting, electronics presentation, cosmetic sets, jewellery and watch packaging, and each use case pulls the specification in a different direction. A protective shipping version wants heavier board and a tighter closure, while a presentation version wants a cleaner face and a softer finish. Understanding which application drives your order is the first brief you give a manufacturer, and it shapes everything from grammage to lead time. A good manufacturer will ask about the item, the market, and the shipment before quoting, because those three facts decide most of the cost. A rigid box manufacturer project moves faster when you confirm the board grade, the print, and the closure before sampling begins.
Treat the first conversation as a specification session, not a price hunt, and the quote you receive will be one you can actually build a programme around. The manufacturer also owns the dieline, so every reorder reuses the same tooling and the same result, which protects your brand across seasons. For brands weighing where to source, the manufacturer relationship is the one that compounds in price and quality over time, and the one hundred piece minimum is simply the on ramp to that relationship rather than a one off commitment.
Material and Grammage Standards
The material choice defines both the feel and the freight for rigid boxes. Rigid boxes built from 157 gram face paper over 1200 gram greyboard give the weight and edge crispness that premium items expect, and they ship assembled. Folding cartons in 300 to 500 gram paperboard are lighter and ship flat, which suits high volume programmes where the box is packed at a fulfilment centre rather than presented in store. Kraft options lean natural and work for brands with a craft or sustainable story. The constraint is that everything stays in the paper and paperboard lane, which keeps you clear of the non paper substrate red line and controls cost.
For most rigid boxes, rigid is the right answer for hero pieces and folding is the right answer for everyday volume. Specify the grammage explicitly in the brief, because a vague request for cardboard means different things to different factories and leads to inconsistent results between runs. A manufacturer that has run seasonal programmes will show you the board range and explain where each grade binds on cost versus durability. Ask for a physical swatch of the proposed board before sampling so the hand feel is confirmed, not assumed, and the proof later validates a material you have already touched. Most rigid box manufacturer buyers start with one sample, then scale once the dieline and the print setup are approved.
The board grade is the largest single cost line on the order, so the few minutes spent confirming it protect the margin on every unit in the container. A manufacturer who walks you through the grade choices without defaulting to the most expensive option is one thinking about your repeat business. Keep the approved swatch and grade on file so every reorder matches, because colour and stiffness drift between unnamed stocks is the quiet source of most box complaints.
How Rigid Boxes Are Made
The production path for rigid boxes starts with the dieline, the knife that cuts and scores the board into the box shape. From there the face paper is printed, the board is laminated or coated, and the structure is folded and glued. For rigid boxes the greyboard is wrapped with the printed face; for folding cartons the flat sheet becomes a shippable blank. Each step is a chance for a pass or a misregistration, which is why setup and proofing matter more than the raw board price. A manufacturer with stable finishing since 1998 can hold tolerances across a large run, and that consistency is what protects you from a one in twenty defective box.
The make ready, the setup that prepares the press and the cutter, is the fixed cost that volume spreads. That is why the one hundred piece minimum is the entry and why the unit price steps down as quantity rises. Understanding the make ready also explains the reorder advantage: once the dieline and print setup exist, a replenishment order skips part of the setup and comes back faster and cheaper. A manufacturer should be able to explain this clearly, and if they cannot, that is a signal about how transparent the rest of the relationship will be. The right rigid box manufacturer spec balances board weight, print finish, and shipping size for your retail or ecommerce channel.
The finishing stage is where seasonal experience shows. A plant that has run holiday and peak programmes knows which foils scuff, which glues relax in humidity, and which scores crack in cold transit. That institutional memory is worth more than a slightly lower board price, because it is what keeps your container consistent from the first carton to the last. Ask the manufacturer how long they have run your box type, not just how long they have existed.
Sizes, Dielines, and Custom Dimensions
Custom dimensions are the whole point of working with a manufacturer rather than a stock supplier. For rigid boxes, the internal size should be driven by the product plus a small tolerance, not by a round catalogue number, so the item sits without rattle and the closure meets cleanly. Send the real product, or an accurate mock, so the dieline is cut to the actual footprint rather than a guess. A dieline built around the real item is what prevents the most common failure, which is a box that looks right on paper and fits badly in the hand.
Keep the approved dieline on file with the manufacturer so every reorder starts from the same geometry. Because the dieline persists, a small first run this season becomes a faster, cheaper reorder next season, which makes the minimum order a foundation rather than a one off cost. If you sell several product sizes, consider a shared footprint with different inserts so one dieline serves a range and the setup cost is spread even further. The dieline is the asset; treat it like one. For a rigid box manufacturer run, share the fill weight and the shelf context so the structure and the insert are matched to the product.
When you brief the factory, give the external size you want on the shelf and the internal size the product needs, because the board thickness consumes part of the external dimension. A manufacturer who confirms both numbers with you is one who understands that the box must look right in the hand and fit right on the shelf. Get this written into the dieline approval so the bulk run cannot drift from the sample.
Printing, Foil, and Finish
Rigid boxes carry brand identity mostly through print and finish. Confirm the Pantone or CMYK target before sampling and insist on a physical proof so the foil and the paper are seen together under real light. A single foil line, a debossed logo, or a soft touch coating is usually enough to signal premium; a busy box with several processes looks cheaper because the eye reads the effort as clutter. Keep the finish count modest so the box can be produced consistently across a large run, because a foil that misregisters on one in twenty is a return waiting to happen.
If you sell in several markets, keep the design language consistent so the range looks like one brand across the shelf. The proof is where identity is confirmed, so never skip it to save a few days, especially on a hero product where the open moment is the brand moment. A manufacturer with experienced seasonal finishing will flag finish choices that are hard to hold at volume, which saves you from a specification that looks good in a sample and fails in a container. Sourcing rigid box manufacturer from a dedicated line keeps the dieline, the print, and the lead time consistent from sample to bulk.
Finish also interacts with transit. A UV coat hardens the surface against scuff in the courier network, while an uncoated soft touch feels premium but marks more easily, so the choice depends on whether the box ships assembled or in a secondary carton. Talk through the journey with the manufacturer, because the finish that wins on the shelf is not always the finish that survives the sea. The right answer is specific to your shipment, not to a catalogue swatch.
MOQ, Sampling, and Bulk Lead Time
The minimum order quantity for rigid boxes starts from one hundred pieces, which lets a brand test a design without a large commitment. Larger volumes reduce the unit cost through setup spread, and a committed seasonal total across splits can unlock a better tier even if you ship in two or three deliveries. Talk to the factory about your total volume, not just your first carton, because the committed number is what moves the price.
The safe order pattern is sample, then bulk, then top up. Sampling takes only a few days once the product and the dieline are confirmed, and it is the moment to validate the structure and the print against a physical proof. After approval, bulk production runs ten to twenty working days. The mistake brands make is one giant late order instead of a small first run plus a replenishment, because the peak compresses production and freight together. A first order validated by a proof, followed by a top up, keeps you in stock without betting everything on a single slot. When you plan a rigid box manufacturer order, send product dimensions, target market, and a print reference so the factory returns a dieline and a proof quickly.
The reorder advantage compounds the rhythm. Because the setup persists, the top up after your first run is faster and cheaper than the first run was, and the sales signal from the first run tells you how much to commit. That loop is what turns a one hundred piece test into a confident programme, and it is the single most useful habit a new brand can build with a manufacturer. Plan the first order early so the top up lands before the peak, not during it.
Cartons, Freight, and Shipping
Boxes are packed one hundred pieces per carton kept at or under twenty two kilograms, which keeps handling standard and container packing efficient. For rigid boxes the box size usually binds before the weight cap does, so confirm the count per carton explicitly in writing so the freight quote matches the box. Ocean freight from a Dongguan factory to the United States or Europe takes several weeks depending on the port and the season, so plan the first order well ahead of the selling window.
Air freight exists for late top ups but erodes margin at box volume, so reserve it for emergencies rather than the main run. Rigid boxes ship assembled and take more warehouse room than folding cartons, which ship flat and save space until pack out. Because the dieline and print setup persist after the first run, a reorder the following season is faster and cheaper, which makes a small test this year a foundation for next. Plan the carton size with the factory for efficient container packing rather than accepting a default. A rigid box manufacturer project moves faster when you confirm the board grade, the print, and the closure before sampling begins.
Freight planning is part of the box specification, not an afterthought. Tell the manufacturer your destination port and your desired arrival window, and ask for a carton size that packs the container tightly without exceeding the weight cap. A few millimetres of box size can change how many cartons fit per container, and that difference is real money on a full shipment. The manufacturer who helps you optimise the carton for the container is saving you freight on every reorder.
Quality Checks and Common Mistakes
A rigid boxes fails loudly when the structure collapses or the print misregisters. Before bulk production, pull a random carton from the run rather than a hand picked sample so you see production quality, not a showcase piece. Check that the board scores cleanly, that the glue holds under a light pull, and that the closure meets square. These checks take an afternoon and prevent a late, defective shipment that cannot be reprinted before the season.
The common mistakes are predictable: quoting on size alone without confirming the insert, skipping the physical proof to save a few days, and placing one oversized late order instead of a tested first run plus a top up. It is also worth opening a shipped carton on arrival, not just at the factory gate, because transit can reveal issues the static check missed. A manufacturer that welcomes these checks is one you can build a programme with, and one that resists is one to avoid. Most rigid box manufacturer buyers start with one sample, then scale once the dieline and the print setup are approved.
Document the checks and feed the results back to the factory, because the loop is what keeps the next reorder clean. A random carton pulled mid run, an arrival inspection, and a short note on what to hold are the three habits that separate a brand with consistent packaging from one that gambles on every container. The cost of the checks is an afternoon; the cost of skipping them is a season of returns.
FSC Ready Paper and Compliance
FSC ready paper is available with chain of custody documents on request, which matters for brands with a sustainability claim or a retailer that requires certified stock. Confirm the requirement before sampling so the correct paper is ordered and the documents travel with the shipment. The factory in Dongguan has operated since 1998, which means the paper supply and the finishing experience are stable across seasonal peaks.
For international brands, document the material and the origin so the customs entry is smooth, and keep the certificate on file for buyer audits. A certified stock also lets you state the claim honestly on the product page, which is increasingly what a buyer looks for. The cost uplift for FSC ready paper is modest at volume and is usually worth it for the audit trail alone, especially when a single audit can unlock a large recurring order.
Compliance is a maintained document trail, not a one time checkbox. Wholesale and retail buyers are exactly the ones who ask for it, so keep the chain of custody current and tied to the specific order, not just to a generic mill certificate. A manufacturer who understands this and supplies order specific documents is one who will keep clearing your shipments through customs without drama.
Magnet Strength and UV Finish
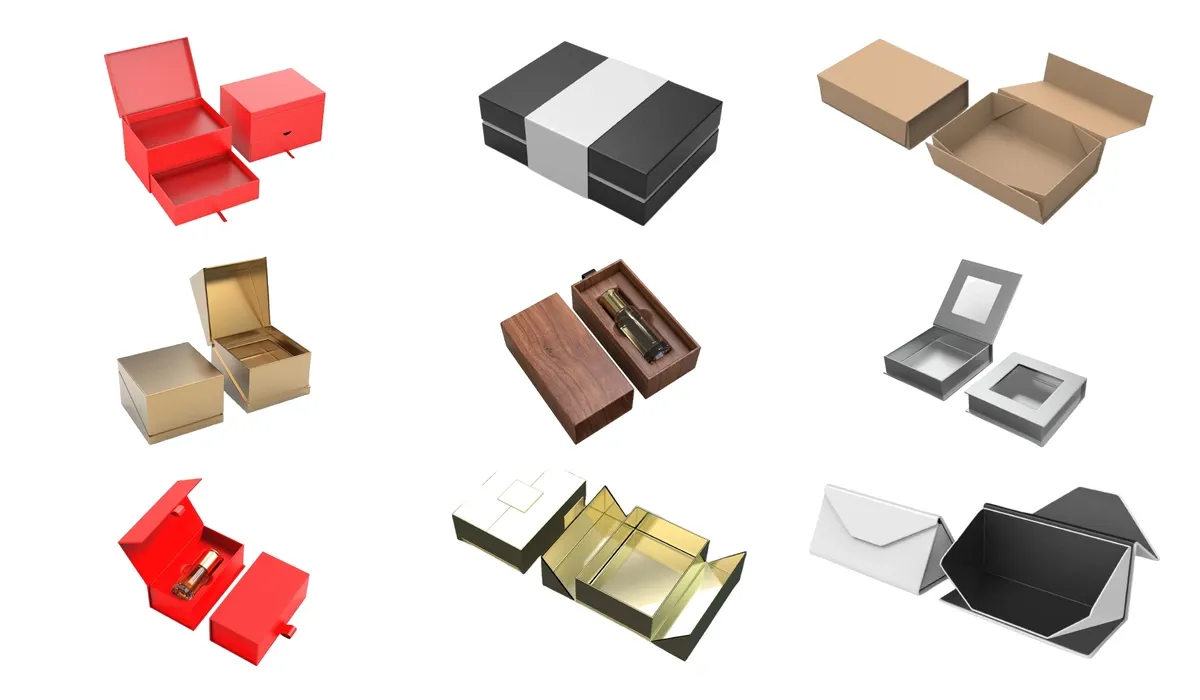
Rigid boxes are defined by the wrap and the closure. The standard is 157 gram face paper over 1200 gram greyboard, which gives the weight and crisp edge that premium items expect. A magnetic closure adds the satisfying snap, and a UV or soft touch finish protects the print and signals quality. The magnet strength should be confirmed on a proof, because a weak close undermines the whole premium impression.
UV coating hardens the surface against scuff during transit and handling, which matters for a box that ships assembled. A manufacturer should explain how the finish interacts with the foil so the two hold together across a large run. The closure and the finish are the details that separate a confident gift from a wobbly one, so specify them, do not leave them to chance.
The wrap itself deserves attention: the face paper weight and the lamination set how the box ages on a shelf. A thin face on a heavy board can crack on the corners; a well matched wrap stays crisp. Ask the manufacturer for the face and board combination they recommend for your item weight, because the rigid box is a system, and the system is only as strong as its weakest layer.
Working With a China Factory: A Practical Brief
The practical way to start a rigid boxes programme is to send the manufacturer three things: the real product, the target market, and the shelf or ship context. With those, the factory can propose the board, the dieline, and the finish that fit, rather than quoting a default and hoping it works. The one hundred piece minimum means you can test that proposal for a modest sum before committing the season.
Confirm the proof schedule in writing, agree the carton size and count, and ask for a price break table at several quantities so you can plan the first run and the top up against known costs. Sampling takes only a few days and bulk runs ten to twenty working days, so the calendar is predictable once the dieline is set. The factory in Dongguan has operated since 1998, which is the stability you want behind a peak order.
Keep every approved artefact, the dieline, the swatch, the proof, and the certificate, on file so reorders are faster and cheaper and never restart the design conversation. That archive is the compounding asset of the manufacturer relationship, and it is what lets a small test this year become a confident, lower cost programme next year. Send the brief, get the proof, and plan the rhythm.
FAQ
What is the minimum order for rigid boxes?
The minimum order quantity starts from one hundred pieces, which lets a brand test a premium style without a large commitment.
What is the standard construction?
Rigid boxes use 157 gram face paper over 1200 gram greyboard, which gives the weight and crisp edge premium items expect.
What closures are available?
Magnetic closures, drawer boxes, flip tops, and lift off lids. Confirm the magnet strength on a proof before bulk.
How long does sampling take?
Sampling takes only a few days once the product and the dieline are confirmed. The proof validates the closure and the print.
What is the bulk lead time?
After sample approval, bulk production runs ten to twenty working days. A small first order plus a top up protects stock.
Do you offer UV and foil finishes?
Yes. UV hardens the surface against scuff and pairs with foil for identity. Keep the finish count modest for run consistency.
How are rigid boxes packed?
Boxes are packed one hundred pieces per carton kept at or under twenty two kilograms. Rigid boxes ship assembled.
Where is the factory located?
Manufacturing is based in Dongguan, China, with operations established since 1998, supporting stable paper supply and finishing.
Can the dieline be reused?
Yes. The approved dieline is archived so every reorder starts from the same geometry and result.
Conclusion
Rigid boxes succeed when the specification matches the product, the material signals the right price tier, and the order rhythm keeps you in stock. Choose rigid 157 gram face paper over 1200 gram greyboard for hero pieces and folding 300 to 500 gram paperboard for volume, send your real items so the cavities and dielines are cut to fit, and use one strong foil for identity. Sample in only a few days, bulk in ten to twenty working days from a Dongguan factory with one hundred pieces since 1998, and keep the setup on file for a faster reorder. Send your product types and your target market, and we will return a dieline, a proof, and a landed timeline you can plan against, so the first order is a confident step into a programme rather than a guess.